Top 10 Benefits of Double Sided PCB Board for Global Buyers?

Time:2026-09-05 Author:Isabella
0%

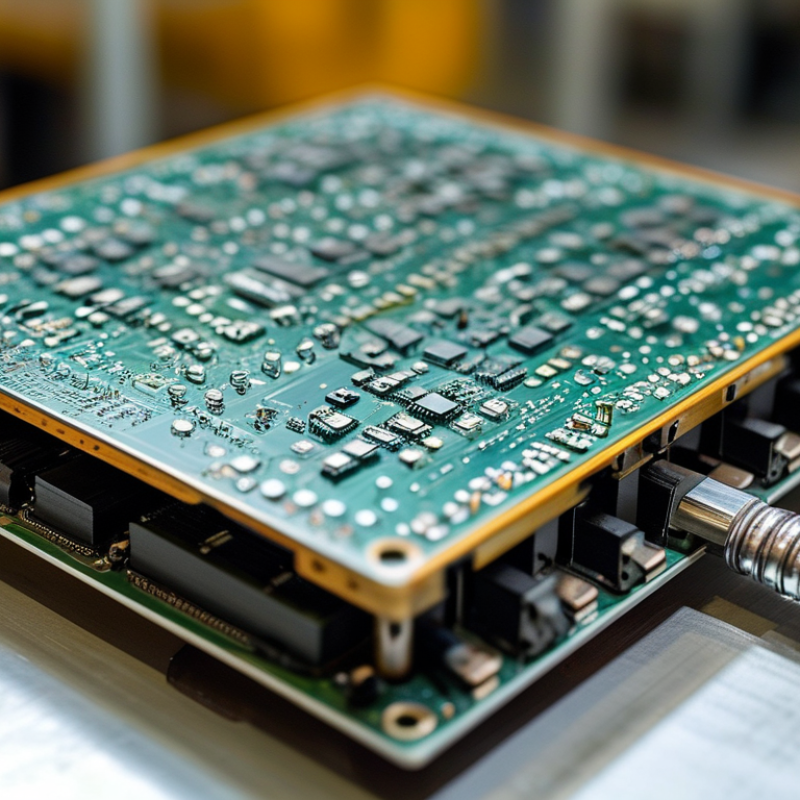
The Double Sided PCB Board offers numerous advantages for global buyers looking to enhance their electronic products. This technology allows for a compact design, making devices smaller and more efficient. By utilizing both sides of the board, manufacturers can optimize space and improve circuit performance. This layout supports complex designs, leading to better functionality.

Moreover, Double Sided PCB Boards enable higher component density. This feature is crucial in today’s technology-driven world, where miniaturization is essential. However, some buyers may struggle to manage the increased complexity of these boards. Understanding material specifications and fabrication processes is vital. Ensuring you select the right supplier can mitigate potential issues.

Lastly, the reliability of Double Sided PCB Boards cannot be overlooked. Their robust construction often leads to longer lifespans and reduced failures. Yet, sourcing quality boards requires careful evaluation of manufacturers. Identifying trusted suppliers with a track record of excellence is critical for buyers. These factors make Double Sided PCB Board a pivotal choice in modern electronics.
Top 10 Benefits of Double Sided PCB Board for Global Buyers?

Benefits of Enhanced Circuit Density in Double Sided PCBs

Double-sided printed circuit boards (PCBs) offer significant advantages, particularly in circuit density. A 2022 report from the IPC highlights that engineers can achieve up to 30% more circuit density with double-sided designs compared to single-sided options. This increased density is crucial in devices where space is limited.

Enhanced circuit density doesn't just mean fitting more components. It also reduces the overall footprint of devices, allowing manufacturers to create slimmer and more compact products. For example, a study from the IEEE suggests that optimizing circuit layouts can lead to improved thermal performance and reduced electromagnetic interference. This dual benefit is vital in modern electronics, where performance and miniaturization are key.

However, designing double-sided PCBs presents challenges. Engineers must navigate more complex routing for traces. The risk of errors increases with density, which can lead to potential reliability issues. Continuous testing and iteration are necessary to ensure durability under various conditions. Balancing density with reliability is an ongoing challenge in PCB design, requiring skilled expertise and careful planning to achieve optimal results.

Improved Signal Integrity and Reduced Noise in Complex Designs

Double-sided PCB boards have gained significant popularity among global buyers. One key advantage is improved signal integrity. In complex designs, maintaining the quality of signals is crucial. Studies reveal that double-sided PCBs can reduce signal loss by up to 30%. This reduction leads to more reliable electronics, especially in high-frequency applications.

Noise reduction is another vital benefit. By utilizing both sides of a PCB, engineers can effectively separate power and signal lines. This separation minimizes electromagnetic interference (EMI), enhancing overall performance. Some reports suggest that well-designed double-sided boards can lower noise levels by approximately 20 dB. Such improvements can be critical in communications and data transfer technologies, where clarity is essential.

Despite these benefits, challenges remain. Designing double-sided PCB layouts requires expertise. There is the risk of increased manufacturing complexity. Engineers must ensure precise alignment for effective signal routing. Additionally, while double-sided boards can reduce noise, they are not immune to it. Understanding these nuances is essential for making informed decisions.

Top 10 Benefits of Double Sided PCB Board for Global Buyers

Benefit Description Impact on Design
Improved Signal Integrity Reduces electromagnetic interference and enhances signal quality. Crucial for high-frequency applications and sensitive data transmission.
Reduced Noise Lower noise levels contribute to more reliable circuit performance. Enhances overall performance in complex designs.
Space Efficiency Allows for compact designs by utilizing both sides of the board. Ideal for devices with limited space.
Cost-Effectiveness Potential for reduced manufacturing costs due to minimized material usage. Suitable for mass production without compromising quality.
Heat Dissipation More efficient heat distribution across the board. Essential for power-intensive applications.
Flexibility in Design Offers greater versatility in schematics and layout options. Encourages innovative designs in electronics.
Enhanced Component Placement Facilitates better placement of components for optimal performance. Improves accessibility and reduces layout complexity.
Aesthetic Appeal Offers a cleaner look for consumer electronics. Increases consumer attraction and brand value.
Improved Reliability Minimized risk of defects and failures. Critical for mission-critical applications.
Longer Lifespan Robust construction leads to increased longevity of the board. A major advantage for industrial applications.

Cost-Effectiveness of Double Sided PCBs for Global Manufacturing

Double-sided printed circuit boards (PCBs) offer significant cost-effectiveness for global manufacturers. By utilizing both sides of the board, they allow for more components in a smaller space. This efficient design reduces material costs and can decrease assembly time. Manufacturers appreciate this efficiency as it leads to lower production costs. The intricate layering also enhances performance and can reduce weight, which is crucial in many industries, from automotive to consumer electronics.

When considering double-sided PCBs, evaluate the total production process. While the boards save costs, unforeseen issues can arise. Quality checks and precise soldering must be prioritized to prevent failures. Investing in high-quality materials, despite a higher upfront cost, often leads to long-term savings. It's worth noting that some manufacturers overlook these critical elements, impacting overall reliability.

Manufacturers should also consider potential scalability. As production scales, the advantages of double-sided PCBs become more pronounced. Efficient designs lead to faster production cycles. Yet, it’s essential to keep communication open between design and manufacturing teams. Discrepancies in design specifications can lead to costly revisions down the line. Taking these factors into account can drastically improve the outcome of PCB projects.

Top 10 Benefits of Double Sided PCB Board for Global Buyers

Increased Thermal Management and Reliability in Electronic Components

Double-sided PCB boards have gained popularity due to their enhanced thermal management capabilities. With components placed on both sides, heat dissipation improves significantly. This is crucial in high-performance electronics, where excess heat can cause failures. By distributing heat more evenly, double-sided PCBs help maintain operational integrity.

Reliability is another key benefit. These boards often feature more robust connections and reduced signal interference. The compact design can minimize the risk of physical damage. However, the production process can be complex. Manufacturers must ensure precise alignment and soldering to avoid defects. Small variations in thickness can lead to issues during assembly.

Thermal management is not just about heat; it also affects component lifespan. Proper heat distribution prolongs the life of sensitive electronics. However, challenges remain. Engineers must carefully consider material selection and board layout. Balancing these factors is essential for optimal performance. Such considerations highlight the importance of expertise in PCB design and production.

Flexibility in Design and Application Versatility for Buyers

Double sided PCB boards offer significant flexibility for design and application. Their ability to accommodate complex circuitry makes them ideal for a variety of devices, from consumer electronics to industrial machinery. This versatility allows manufacturers to optimize space and enhance functionality while keeping costs manageable.

Designers can lay out components on both sides of the board, maximizing the surface area. This leads to smaller devices and improved performance. The flexibility in routing signals can also reduce electromagnetic interference, which is vital for sensitive applications. However, integrating these boards requires skilled professionals who understand the nuances of double sided layouts.

When choosing materials, consider the thermal properties of your project. In some cases, improper material selection can lead to overheating, which affects performance and longevity. Reviewing thermal management strategies can provide significant advantages. Remember, the PCB design process requires collaboration among engineers, ensuring all aspects are well-addressed.

Reflecting on past projects can highlight areas for improvement. Not every design yields perfect results, and learning from mistakes is key to success. Strive for innovative solutions, but remain mindful of practicality. Balancing these factors will ultimately lead to better design outcomes.

FAQS

: What is a main advantage of double-sided PCBs?

: Double-sided PCBs can achieve up to 30% more circuit density than single-sided designs.

How does enhanced circuit density affect product design?

It allows manufacturers to create slimmer and more compact products, saving space.

What is one thermal advantage of double-sided PCBs?

They can lead to improved thermal performance and reduced electromagnetic interference.

What challenges do engineers face when designing double-sided PCBs?

They must manage complex routing and a higher risk of errors, which can impact reliability.

How do double-sided PCBs improve signal integrity?

They can reduce signal loss by up to 30%, leading to more reliable electronics.

In what way does noise reduction occur in double-sided designs?

Engineers can separate power and signal lines, minimizing electromagnetic interference.

What is the potential downside of double-sided PCB designs?

Increased manufacturing complexity can make the process more challenging.

Why is testing critical in the design of double-sided PCBs?

Continuous testing ensures durability and reliability under various conditions.

Can double-sided PCBs eliminate all noise?

No, while they reduce noise, they are not immune to it; understanding this is key.

Is expertise important in double-sided PCB design?

Yes, skilled expertise is essential for effective layout and signal routing.

Conclusion

The "Top 10 Benefits of Double Sided PCB Board for Global Buyers" highlights several key advantages that improve circuit design and manufacturing efficiency. One of the primary benefits is enhanced circuit density, which allows for more compact and efficient designs, essential for modern electronics. Additionally, double sided PCBs offer improved signal integrity and reduced noise, making them ideal for complex applications.

Cost-effectiveness is another significant advantage, as these boards streamline production processes for global manufacturing. Furthermore, double sided PCB boards provide increased thermal management and reliability, ensuring that electronic components operate effectively under various conditions. Lastly, the flexibility in design and application versatility makes them an attractive option for buyers seeking innovative solutions in the ever-evolving electronics industry.

Isabella

Isabella

Isabella is a dedicated marketing professional with a sharp focus on driving brand growth and engagement through strategic content creation. With an extensive background in digital marketing, she combines her passion for storytelling with her keen understanding of industry trends to deliver......